Case Study
Centralised HFO cooling system for a new milk-processing plant
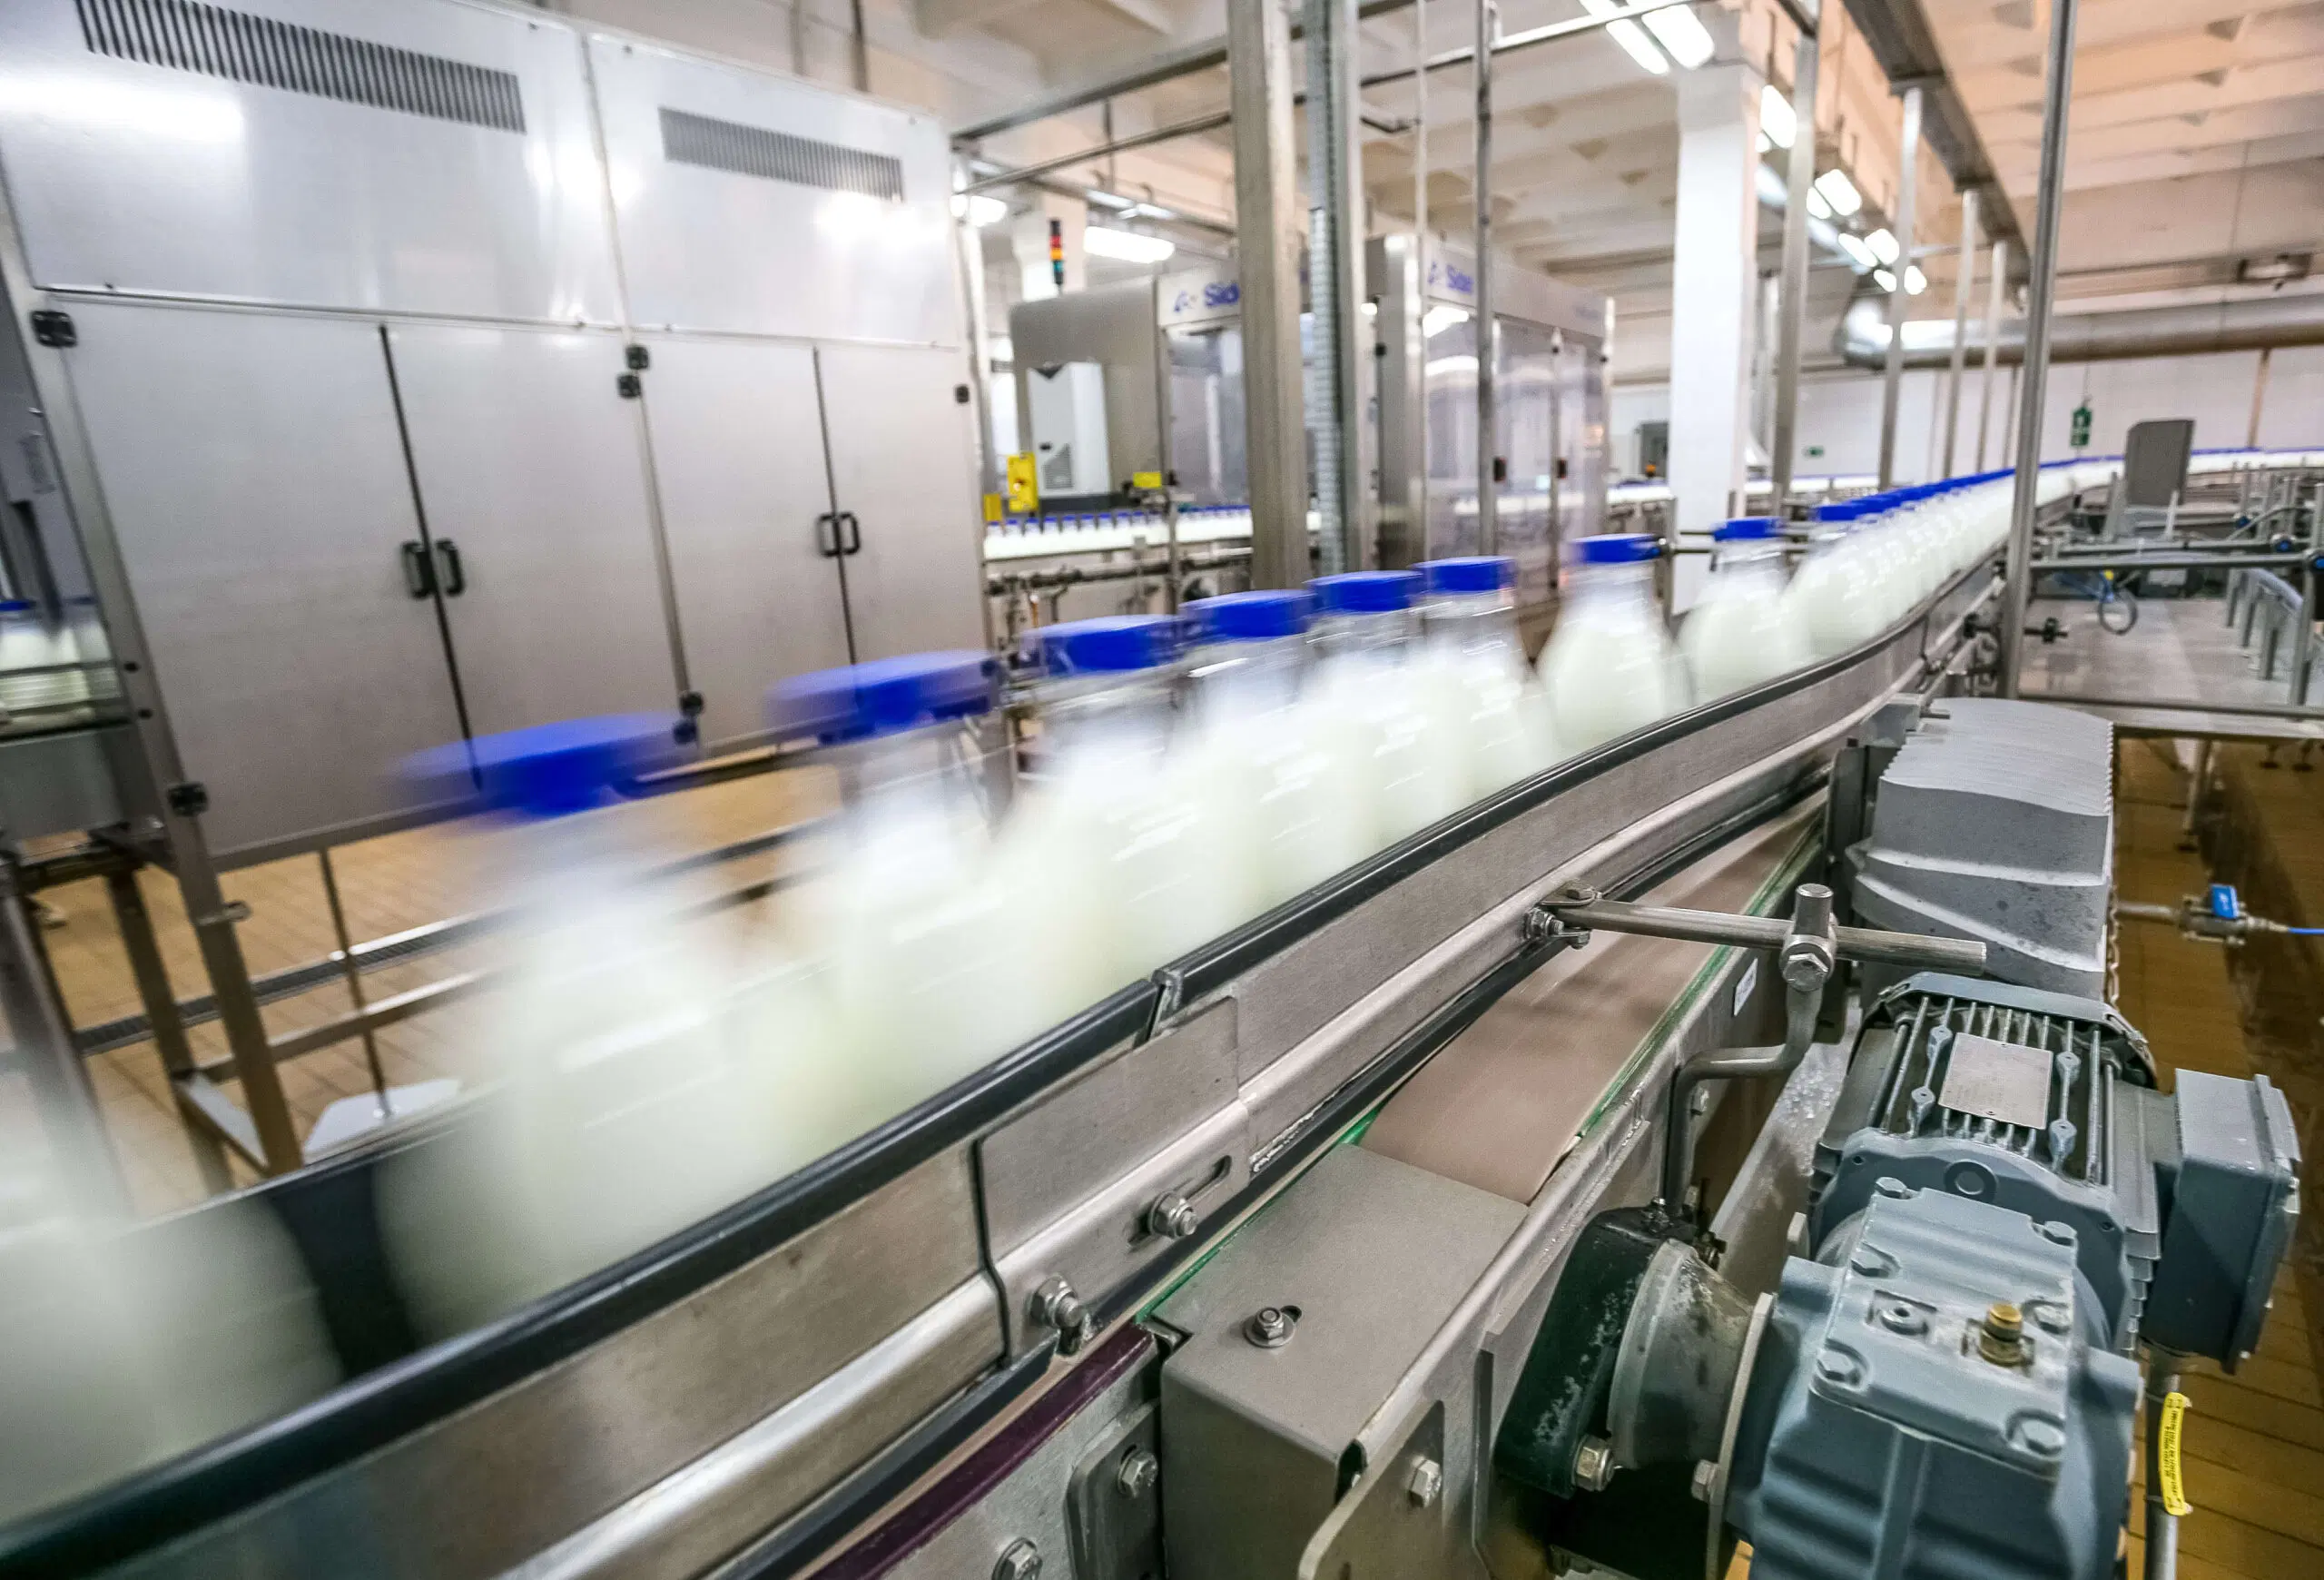
In the dairy industry, precise thermal control is crucial to guarantee product quality while optimising energy consumption. For its new plant, a dairy processor chose an innovative cooling solution using HFO refrigerants, combining performance with environmental responsibility.
MTA designed and installed a bespoke system, delivering perfect thermal control for the various processes while reducing the carbon footprint.
Context
A major player in the dairy sector was building a new processing unit requiring a high-performance centralised cooling system. The objectives were twofold:
- Maintain precise temperatures for various processes (pasteurisation, storage, etc.)
- Adopt an environmentally friendly solution compliant with the latest refrigerant regulations
Solution
MTA deployed a centralised cooling system using HFO refrigerants (hydrofluoroolefins), offering:
- Excellent energy efficiency
- Very low environmental impact (reduced GWP)
- The ability to meet variable cooling demands
The installation comprises:
- High-performance refrigeration units
- An optimised distribution network
- An intelligent control system for precise temperature management
Result
The solution delivered:
- A reduced environmental impact thanks to HFO refrigerants
- Significant energy savings compared with traditional systems
- Perfect thermal control for all milk-processing operations
- Full compliance with current and future regulations